
A gift distributor in the Gulf took delivery of eleven thousand handmade Vietnamese quilling cards last spring. The cards were beautiful, the cartons arrived square and dry, and the customs file cleared without a single query. Six weeks later the stock was still sitting in the warehouse. The three retail chains that had agreed to trial the range each asked the same two questions before they would release a delivery slot: can it be scanned at the till, and can it go onto the fixture in the condition it arrives? The answer to both was no. Re-sleeving, labelling and ticketing eleven thousand cards in-market cost more than the ocean freight had.
Landed is not the same as sellable
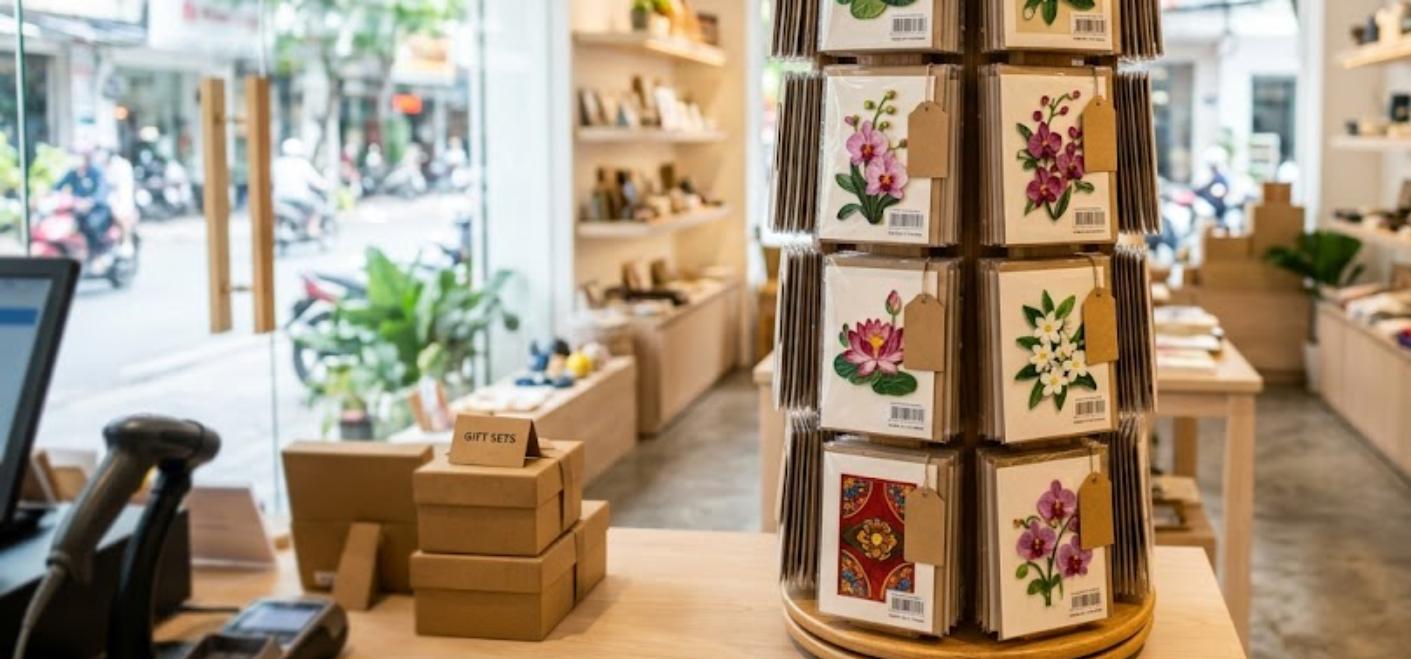
Most sourcing conversations about handmade paper cards stop at the product. Buyers specify the paper weight, the quilling density, the envelope, the blank interior, the carton count. All of that matters, and we have written elsewhere about how those choices drive the unit price. What routinely goes unspecified is everything that happens between the carton being opened and a shopper picking the card up: the sleeve, the barcode, the back-of-card print, the hangtag, the ticket, the fixture and the pack ratio.
That gap is where margin quietly disappears. A retailer who receives a carton of loose, unbarcoded cards has to absorb a handling cost that was never in your quotation. Depending on the market, in-store or third-party labelling of a greeting card runs somewhere between four and twelve US cents a unit once labour, consumables and the second touch of the stock are counted. On a card landing at sixty cents, that is a meaningful slice of somebody’s margin, and it is almost always taken out of yours at the next price negotiation.
The good news is that retail readiness is cheap at origin and expensive anywhere else. Sleeving, barcoding and ticketing a card in a Vietnamese workshop, as part of the finishing sequence, typically adds one to three cents. The same work in a European or Gulf distribution centre costs five to ten times that. Every retail-readiness decision you push upstream into the purchase order is a decision you buy at Vietnamese finishing rates rather than at destination-market labour rates.
This guide walks through the seven specifications that most often go missing, in the order a card encounters them.
1. Start with the sleeve, because everything else attaches to it
A quilling card is a three-dimensional object made of paper. It cannot be merchandised naked. The sleeve is not optional packaging, it is the structural element that lets the card survive being handled by fifty shoppers without the quilled coils being crushed or soiled. It is also the surface that carries your barcode, so the sleeve decision comes first.
Three formats dominate, and they are not interchangeable.
- Crystal-clear polypropylene sleeve with a resealable lip. The retail default. Holds card and envelope together, shows the quilling at full contrast, accepts a label cleanly. Specify 30 to 40 micron film: thinner tears at the till, thicker looks cheap and creases white.
- Cellophane, cellulose-based and home compostable. The same optical clarity, a genuine end-of-life story, roughly twenty to thirty per cent more expensive and less tolerant of humidity in transit. Worth it for ranges positioned on sustainability, but it must be paired with the moisture control described in our guide to packaging and protection for export shipping.
- Paper band or belly wrap, no film at all. Increasingly requested by plastic-free retailers. It looks excellent and it protects almost nothing, so it only works where the card also sits in a rigid tray or a fitted box.
Two details are worth arguing about at sample stage. First, whether the sleeve is sealed or resealable: sealed sleeves protect better and frustrate shoppers who want to see the inside of the card, and in the gift trade a card that cannot be opened is a card that does not convert. Second, the suffocation warning. Many retailers require a printed warning on any film bag above a certain size; check your buyer’s vendor manual rather than assuming, because thresholds and wording differ by chain and by market.
2. Barcodes: the detail that stops a till lane
Who owns the number
This is the single most common point of confusion, and it has a simple answer: the brand owner allocates the GTIN. If the cards carry your brand, your company licenses a company prefix from your national GS1 member organisation and issues a unique number to each design. If the cards carry the manufacturer’s brand, the manufacturer allocates. A supplier cannot lend you their numbers for your own private label range, and a retailer will eventually notice, because the prefix resolves to a different company in the global registry.
Practically, that means the barcode specification cannot be written by your supplier. You send a numbered design list. Every colourway, every size, every multipack is a separate number. A six-card boxed set carries its own number in addition to the numbers on the individual cards inside it, if those cards are also sold singly.
Symbol, size and placement
For retail point of sale outside North America the symbol is EAN-13. North American retail uses UPC-A. Most of our buyers ship into the Middle East, South and Southeast Asia, Europe and Africa, so EAN-13 is the working default, and it scans in North America too.
- Size. GS1 permits EAN-13 to be printed between eighty and two hundred per cent of nominal size for general retail scanning. At one hundred per cent the symbol is roughly 37 mm wide and 26 mm tall including the human-readable digits. Shrinking below eighty per cent to fit a small card is the most frequent cause of a symbol that reads on a handheld scanner in the office and fails on a worn till scanner in a shop.
- Quiet zones. EAN-13 needs a clear margin either side of the bars, wider on the left than the right. Artwork that runs a border, a price box or a decorative rule into that margin will fail verification. On a card sleeve label this is usually solved by giving the barcode its own white panel.
- Colour. Dark bars on a light background, and never red or warm orange bars. Many till scanners read with a red light source, to which red bars are effectively invisible. Do not print bars on kraft, foil, or any dark or metallic stock without testing.
- Height. Do not truncate the bars to save space. Shortened symbols only scan when presented at exactly the right angle, which is not how a queue works.
- Placement. Decide once and hold it across the range. Bottom right of the reverse of the sleeve is the convention in the gift trade, and consistency matters more than the specific corner, because it is what lets a cashier scan without turning the card over twice.
Ask for a scan verification report, not a photograph of a barcode. A printed symbol has a measurable grade, and the difference between a grade that passes and one that fails is often invisible to the eye: ink spread on uncoated stock closing the gaps between bars is the classic failure on handmade ranges, where the label is frequently printed on recycled or textured paper for aesthetic reasons.
Outer cartons need their own symbol. A shipping carton carrying a single product typically uses an ITF-14 printed directly on the corrugate, or a GS1-128 label where the retailer wants batch and quantity data encoded. This is separate from the shipping marks and the documentation covered in our customs and rules of origin guide, and both are required.
3. The back of the card is your cheapest marketing asset
Shoppers turn greeting cards over. They do it to find the price, and while they are there they read whatever else is printed. On a handmade card that reverse panel is the only place the story gets told, and it costs nothing extra because the card is already going through a printing step.
A well-built back panel carries six things:
- Your brand block, at a size that survives being cropped by a price ticket
- One line on the making: that each card is cut, rolled and assembled by hand, and roughly how long it takes
- The country of origin, stated plainly as Handmade in Vietnam
- Material and environmental claims you can actually evidence, with certificate codes where a scheme requires them
- Care and disposal guidance, including how to separate the sleeve from the card
- A design reference code, which is what lets a retailer reorder the design that sold out
Two cautions on the claims. An FSC claim may only appear on product if the certificate holder is certified for chain of custody and the claim is made under a valid licence code. Printing a logo because the paper mill is certified somewhere upstream is a trademark misuse, and buyers with their own certification will catch it during onboarding. Recycled-content percentages are the same: state them only where the figure is supported by the bill of materials described in our post on the compliance evidence pack.
Market-specific marks belong here too, and they change. Buyers placing product on the European market should be tracking the EU Packaging and Packaging Waste Regulation, which becomes applicable during 2026 with harmonised material-composition labelling phased in afterwards, alongside existing national requirements such as the French sorting mark and the various extended producer responsibility registrations. These obligations sit with the party that first places the packaging on the market, which is usually the importer rather than the Vietnamese maker, but the artwork has to be produced in Vietnam, so the information has to travel upstream with the order. Confirm the current wording with your own compliance advisers before the artwork is locked.
A QR code on the back panel is worth considering, and worth restraining. It should resolve to something durable, such as a page describing the craft and the workshop, rather than a campaign URL that will be dead in eighteen months. Cards stay on shelves for years.
4. Hangtags, price tickets and the cost you push onto your retailer
The hangtag is the small kraft or board tag attached to the sleeve or the card itself. On a handmade range it does real work: it signals craft, it separates the product visually from machine-made cards on the same fixture, and it gives the retailer a surface to staple or clip a price ticket onto without marking the sleeve.
Decide four things and write them into the specification:
- Attachment. String, elastic loop, plastic tagging barb or adhesive. Barbs are fast and cheap and are refused by some sustainability-led retailers. String is slow, costs a cent or two of labour, and photographs beautifully.
- Whether the barcode lives on the tag or the sleeve. Putting it on the tag looks cleaner but means a detached tag becomes an unsellable card. We recommend the sleeve for the scannable symbol and the tag for brand and story.
- Pre-ticketing. If your customer wants retail prices printed at origin, that is a separate ticket, a separate artwork file per market and per currency, and it locks your pricing for the life of the production run. Many buyers ask for it and then regret it. A blank ticket panel is usually the better answer.
- Who supplies the tag artwork. If the retailer’s own brand appears on the tag, their studio supplies print-ready files, and those files need to be locked before the golden sample is signed. Our guide to sampling and pre-production approval explains why late artwork is the most common cause of a missed shipping window.
5. Display units: the difference between a shelf and a destination
Handmade quilling cards do not compete with ordinary greeting cards, and they lose when they are merchandised as if they did. Slotted into a standard card wall at a standard price point, a three-dimensional card looks like an expensive anomaly. Given its own fixture, it becomes a category.
Four fixture types cover almost every conversation:
- Counter display unit. A small corrugate or board tray holding twenty-four to forty-eight cards across four to eight designs, sold filled. The workhorse of the gift trade, because it converts an impulse purchase at the till and requires no fixture commitment from the retailer.
- Rotating counter spinner. Timber or acrylic, ninety-six to two hundred cards, four to six faces. Higher investment, much higher sell-through, and the format that turns a trial into a permanent listing. Usually supplied free or at cost against a minimum fill order.
- Floor-standing spinner. Three hundred cards and up. Appropriate for museum and gallery shops, airport retail and garden centres. Ships knocked down and flat, which is its own specification problem.
- Shelf-ready tray. The card carton is designed so that its lower half becomes the shelf tray when the perforated top is removed. No unpacking, no merchandising labour. Increasingly the price of entry with larger chains.
The question that decides the commercial conversation is who pays. Our position, and the one we would recommend to any buyer negotiating with a Vietnamese workshop, is that fixtures should be priced separately and transparently rather than buried in the card price. A spinner amortised invisibly across a first order makes the cards look expensive and makes the reorder, which contains no spinner, look like a price increase.
One practical warning on timber fixtures made in Vietnam: a wooden spinner is a wood product, and it travels under a different classification from the cards it holds, with its own fumigation and packaging-wood requirements in several markets. Do not let a display unit be added to a card order as an afterthought three weeks before shipment.
6. Pack ratios and the mixed-design inner carton
A handmade range lives or dies on assortment. Ten designs sell far more than three, but ten designs also multiply every operational cost: ten artwork approvals, ten golden samples, ten GTINs, ten lines on the packing list, and ten separate risks of one design running late and holding the shipment.
The compromise is the pack ratio. Instead of ordering each design separately, the buyer orders a pre-assorted inner carton containing a fixed mix, and the workshop packs to that mix on the line. A typical structure for a first order is six pieces per design, six designs per inner carton, twelve inners per master carton, which yields a clean 432-piece master and lets a distributor break stock down to a single fixture fill without opening more than one box.
Three rules make pack ratios work:
- The ratio is fixed for the season and written on the purchase order, not agreed by email during production. Changing the mix mid-run is where miscounts enter.
- Every inner carton carries a label stating the mix, the designs inside and the total, so that a warehouse can verify without opening it.
- Best sellers are ordered as straight single-design cartons on the reorder, not as assortments. Assortments are for discovery; straight packs are for replenishment. Getting this backwards is why distributors end up with a warehouse full of the two designs nobody wanted.
7. What retail readiness does to your lead time
Every specification in this guide adds time before production rather than during it, which is the part buyers consistently underestimate.
- GTIN allocation and barcode artwork: one to two weeks, and entirely on the buyer’s side. This is the most common single cause of delay, because it usually has to pass through a team that was not in the sourcing conversation.
- Sleeve and label tooling, including any printed film: two to three weeks from artwork sign-off.
- Hangtag die-cutting and print: one to two weeks, longer if the tag is die-cut to a custom shape.
- Display unit structural sample and print proof: three to four weeks, and longer again for timber.
- Barcode verification on production stock: two to three days, and it must be scheduled before packing, not after.
Run in parallel with card production, none of this extends the shipping window. Run in sequence, because it was raised after the order was placed, it adds four to six weeks. That is the difference between landing a Christmas range in September and landing it in November.
The retail-readiness clause to put in your purchase order
Most disputes about retail readiness are not disagreements, they are omissions. The following list, attached to the order as an annex, removes almost all of them. Adapt the values; keep the headings.
- Primary packaging: sleeve material, micron, seal type, dimensions, and whether the envelope is inside or outside the sleeve
- Symbology: EAN-13, magnification percentage, exact placement, substrate and print method, minimum acceptable verification grade
- GTIN schedule: a numbered list issued by the buyer, one line per saleable unit including multipacks and display units
- Reverse artwork: print-ready files supplied by the buyer, with a named approver and a version number
- Hangtag: stock, size, attachment method, artwork reference, and whether a price panel is printed or blank
- Inner pack: pack ratio by design, inner label content, inner dimensions and weight
- Master carton: count, ITF-14 or GS1-128 specification, shipping marks, and whether the carton is shelf-ready
- Display units: quantity, fill specification, priced as a separate line, with their own approval sample
- Verification: scan report on production stock issued before packing, plus a dated photograph of one sealed inner and one sealed master
It takes an afternoon to write and it is the difference between a container that goes onto a fixture and a container that goes into a rework queue.
Working with Viet Farm Vision
Viet Farm Vision is a Vietnamese OEM manufacturer and exporter of handmade paper quilling and 3D pop-up greeting cards, supplying importers, wholesalers, retail chains, museum and gallery shops and corporate gifting programmes across the Middle East, Asia and other global markets. We treat retail readiness as part of the product rather than as a finishing extra, because a card that cannot be scanned and shelved is a card that has not really been delivered.
- Sleeving, labelling, hangtagging and pre-ticketing carried out in-house as part of the finishing sequence, quoted as separate, visible lines rather than absorbed into the card price
- Barcode artwork placed to the buyer’s GTIN schedule, printed on a tested substrate, and verified on production stock with the scan report issued before packing begins
- Reverse-panel and hangtag artwork produced from buyer-supplied files under a version-controlled approval, with no substitution permitted after the golden sample is signed
- Pack ratios fixed on the purchase order, labelled on every inner carton, and audited against the packing list before the master cartons are sealed
- Counter display units, spinners and shelf-ready cartons developed alongside the range, sampled on their own approval cycle and priced independently of the cards
If you are planning a handmade card range for the 2027 season, the retail-readiness annex is the document to write first. It costs nothing, it is the part your retail customers will judge you on, and it is far easier to agree before a price has been fixed than after.
To discuss a quilling card programme, request the retail-readiness specification template, or arrange samples, contact Viet Farm Vision at info@vietfarmvision.com or through the enquiry form at vietfarmvision.com/contact.