
A Middle East houseware distributor called us in February with a container already on the water and a problem that had no good answer left. Twelve thousand acacia serving boards, inspected by nobody, signed off on a supplier photo set of forty images. When the container opened in Jebel Ali, roughly one board in nine had a hairline check running from the hanging hole toward the edge. Not catastrophic. Not sellable either, not into a retail chain that photographs every returned unit.
The expensive part of that story is not the defect rate. It is that nobody had ever written down what counted as a defect. The supplier’s position, argued in good faith, was that surface checking is a natural characteristic of solid acacia and that the boards met the sample. The buyer’s position, also argued in good faith, was that the sample had no cracks in it. Both were right, because the contract never defined the boundary. There was no inspection standard, no AQL level, no defect classification, and therefore no mechanism to decide who paid.
Pre-shipment inspection is the cheapest insurance in a wooden kitchenware programme. A third-party inspection day in Vietnam runs roughly USD 280 to 400 depending on the agency and the factory location, and that figure does not move much whether the order is 5,000 units or 50,000. On a USD 60,000 container it is well under one percent of order value. On a container that arrives wrong it is the difference between a documented claim and a conversation. This guide covers how inspection actually works on Vietnamese wood factories in 2026, how AQL sampling is set, what a defect classification table for wooden kitchenware needs to contain, the on-site tests that matter for wood specifically, and how to write the inspection clause into your PO so the result is enforceable.
Why Wooden Kitchenware Needs A Different Inspection Approach
Most inspection protocols were written for goods where every unit is meant to be identical. Wood is not that. Grain runs differently across a batch, colour varies between boards cut from the same log, and a natural knot is a feature in one buyer’s spec and a rejection in another’s. An inspector arriving with a generic checklist will either pass everything, because natural variation explains away most findings, or fail everything, because no two pieces match.
There are three failure modes specific to solid wood and engineered wood kitchenware, and a workable inspection protocol has to address all three.
Moisture-driven defects appear after inspection, not during it. A board at 14 percent moisture content passes a visual inspection perfectly. Six weeks later, in a heated European warehouse at 35 percent relative humidity, it splits. This is the single most common cause of wooden kitchenware claims, and a purely visual inspection will never catch it. The inspection must include meter readings, not just eyes.
Finish defects are cumulative and invisible in small samples. Oil finish applied in high ambient humidity cures unevenly. It looks fine on unit one and unit two. Across a 12,000-piece run, a batch cured on one particular rainy afternoon will show blotching, and that batch is sitting somewhere in the middle of the pallets. Sampling has to reach into cartons drawn from across the whole production window, not from the top layer of the nearest pallet.
Dimensional drift happens over a production run. CNC tooling wears. A router bit that cut a 3mm radius on day one cuts something closer to 2.6mm on day nine, and on a utensil set where pieces have to sit in a slotted holder, that difference decides whether the product assembles. Inspecting only the first batch tells you nothing about the last.
The Four Inspection Points And Which Ones You Actually Need
Inspection agencies will sell you four stages. For most wooden kitchenware programmes you need two, occasionally three, and paying for all four is usually a sign the supplier relationship is wrong rather than that the inspection plan is right.
Initial Production Check (IPC). Conducted when roughly 5 to 15 percent of the order is complete. The inspector verifies raw material, confirms the approved sample is physically on the production floor, and checks the first finished units against it. On a first order with a new factory, or on any order with custom tooling, this is worth paying for. It is the only stage where a problem can still be fixed cheaply. On a repeat order of a proven SKU, skip it.
During Production Inspection (DUPRO). At roughly 40 to 60 percent completion. Useful specifically on long runs where dimensional drift or finish-batch variation is the risk, which is to say most CNC-heavy or oil-finished wooden kitchenware above about 15,000 units. Below that volume the production window is usually short enough that the pre-shipment check covers it.
Pre-Shipment Inspection (PSI). Conducted when at least 80 percent of the order is produced and 100 percent is packed, or close to it. This is the non-negotiable one. Every wooden kitchenware order leaving Vietnam should have a PSI, including repeat orders, including orders from factories you trust. It is the stage where the report has commercial teeth, because the goods have not yet shipped and payment leverage still exists.
Container Loading Supervision (CLS). The inspector watches the stuffing. Worth the cost when you are shipping a mixed container with several order references, when cargo is palletised and stow matters, or when you have had a short-shipment or mis-labelling incident before. On a single-SKU floor-loaded container from a factory with a clean history, it is optional.
The practical default for a mid-size buyer running a new wooden kitchenware programme is IPC plus PSI on the first two orders, then PSI alone once the factory has demonstrated consistency, with DUPRO added back for any order above roughly 20,000 units or any SKU with new tooling.
Setting AQL Levels That Match Wooden Kitchenware Reality
AQL, Acceptable Quality Limit, is the statistical framework under ISO 2859-1 that decides how many units an inspector pulls and how many defects allow the lot to pass. The convention across consumer hardgoods is General Inspection Level II with acceptance limits of 0 for critical defects, 2.5 for major and 4.0 for minor. Most buyers copy that line into the PO without thinking about it, and for wooden kitchenware it is usually the wrong line in one specific place.
Here is what Level II sampling looks like in practice on typical order sizes.
| Lot size (units) | Sample size | Major accept / reject at 2.5 | Minor accept / reject at 4.0 |
|---|---|---|---|
| 3,201 to 10,000 | 200 | 10 / 11 | 14 / 15 |
| 10,001 to 35,000 | 315 | 14 / 15 | 21 / 22 |
| 35,001 to 150,000 | 500 | 21 / 22 | 21 / 22 |
Two adjustments are worth making for wood.
Tighten the major limit on food-contact items. For cutting boards, serving boards, bowls and utensils that touch food, a major AQL of 1.5 rather than 2.5 is defensible and most Vietnamese factories will accept it without a price adjustment if it is agreed before quoting rather than imposed after. The reason is not statistical fussiness. It is that a major defect on a food-contact wooden item, a split, a rough splinter-producing edge, a finish that has not cured, is a product the end consumer will return and photograph, and the cost of that event sits far above the cost of the unit.
Leave the minor limit alone, but define minors properly. Buyers who tighten minor AQL on wood almost always regret it, because natural grain variation gets logged as minor and the report fails on cosmetic findings that the buyer would have accepted. The better move is to keep 4.0 and spend the effort on the defect classification table instead, so that acceptable natural variation is explicitly not a defect.
One more mechanism that costs nothing and changes factory behaviour: specify switching rules. Under ISO 2859-1, two consecutive failed lots move the inspection to tightened severity, which pulls a larger sample and lowers the acceptance number. Writing that into the PO signals that repeated failures escalate rather than reset, and it is the closest thing a mid-size buyer has to leverage without threatening the relationship.
The Defect Classification Table Your Spec Sheet Is Probably Missing
This is where the Jebel Ali container went wrong, and it is where most wooden kitchenware disputes are actually decided. An AQL number without a defect definition is arithmetic with no inputs. The inspector has to know what to count.
A workable classification for solid wood kitchenware looks something like the table below. It is a starting point, not a standard, and every buyer should adjust the thresholds to their own retail channel before it goes into a PO.
| Finding | Classification | Threshold |
|---|---|---|
| Through-crack or split of any length | Critical | Zero tolerance |
| Mould, fungal staining, live insect activity | Critical | Zero tolerance |
| Splinter or raised grain capable of skin contact injury | Critical | Zero tolerance |
| Surface check (hairline, not through) | Major | Over 15mm long or over 0.3mm wide |
| Moisture content out of range | Major | Outside agreed band, typically 8 to 12 percent for EU, 6 to 10 percent for Gulf |
| Loose or missing knot | Major | Any loose knot; sound knot over 8mm on a food surface |
| Finish blotching, tackiness or uncured oil | Major | Visible at 60cm under normal light |
| Dimensional deviation | Major | Beyond agreed tolerance, commonly plus or minus 2mm on length, 1mm on thickness |
| Glue line gap on laminated or edge-glued panels | Major | Over 0.2mm visible gap |
| Colour variation between units | Minor | Outside approved colour range samples |
| Sound tight knot within size limit | Not a defect | Explicitly stated as acceptable |
| Natural grain and figure variation | Not a defect | Explicitly stated as acceptable |
| Minor tool mark not detectable by touch | Minor | Over 10mm, visible at 60cm |
| Carton marking error, wrong barcode, missing label | Major | Any occurrence |
| Carton crush, water staining, weak closure | Minor | Structural compromise escalates to Major |
The two rows that matter most are the ones marked “not a defect”. Writing down what is acceptable does more to prevent disputes than writing down what is not, because it removes the factory’s main argument in every wood claim, which is that the buyer is rejecting nature.
Colour is worth its own paragraph. The correct control is not a written description but a physical set of range samples, typically three boards representing the lightest acceptable, the mid-tone target and the darkest acceptable. One set stays at the factory, one with the inspection agency or the buyer. Without range samples, “colour variation” is unenforceable, and every acacia programme produces colour variation.
On-Site Tests That Belong In A Wooden Kitchenware PSI
A visual AQL count is only half of a useful inspection. These are the physical checks worth naming explicitly in the inspection booking, because an inspector will only run what the booking asks for.
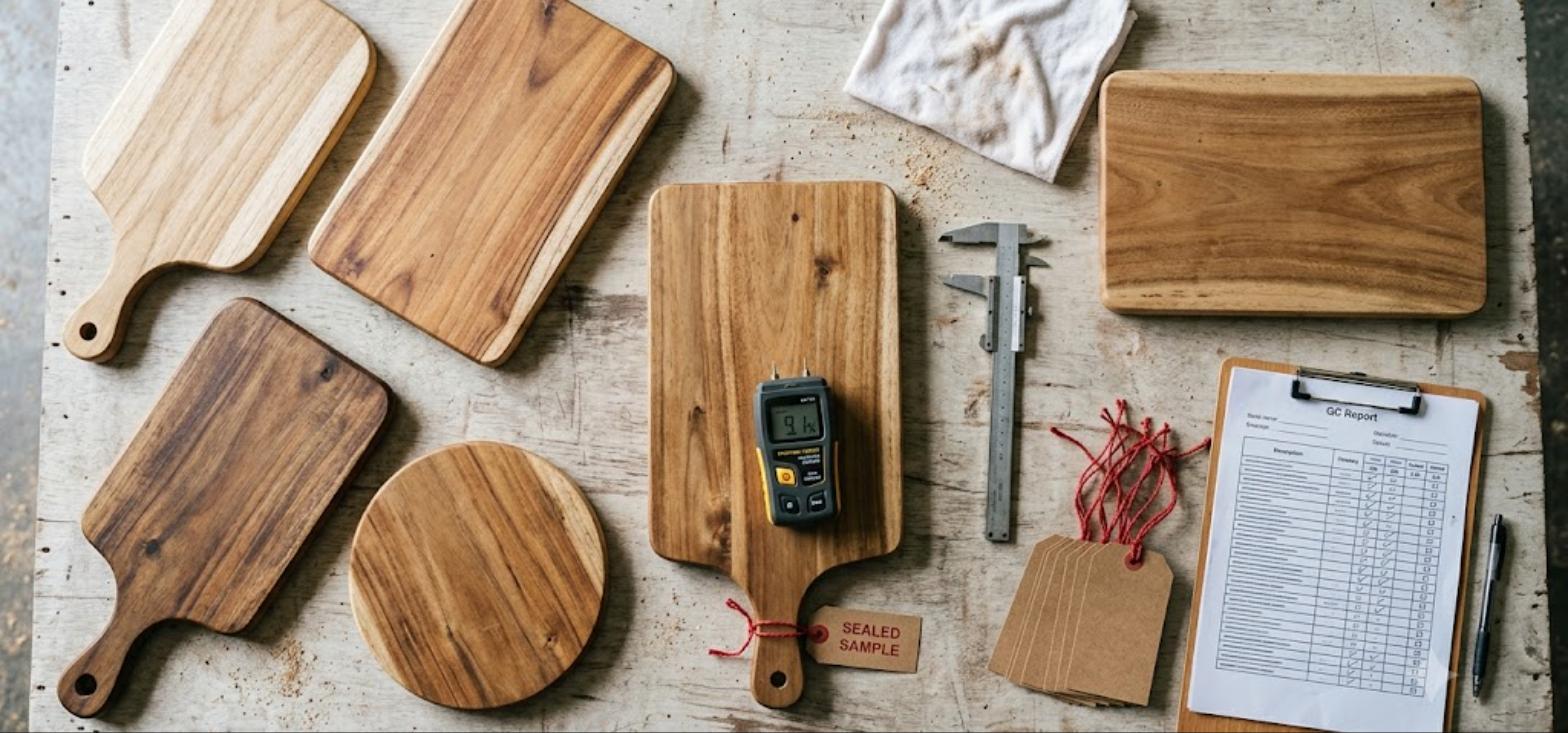
Moisture content, pin meter, minimum ten readings per lot. Readings taken at the thickest cross-section, not the edge, and recorded individually in the report rather than averaged. An average of 11 percent hides a board at 16. For EU and North Asian destinations the usual target band is 8 to 12 percent; for Gulf and desert-climate destinations 6 to 10 percent is safer. Specify the band, do not leave it to the factory.
Carton drop test. Standard protocol is a single carton, ten drops, one corner, three edges, six faces, from 80cm for cartons under 10kg and 60cm above that. The pass criterion is no damage to the product inside; carton scuffing is expected. This single test catches most of the transit damage that would otherwise arrive as a claim.
Finish adhesion and rub test. A dry cloth rub and a damp cloth rub, twenty strokes each, checking for colour transfer or finish removal. On oiled wood this is the practical test for whether the finish has actually cured or was applied the previous evening to hit the shipping date.
Function and assembly test. On utensil sets, holders, boxes and anything with moving or fitting parts, a sample assembly of at least five sets drawn from different cartons. This is where CNC drift shows up.
Weight and dimension verification against the packing list. Carton gross and net weight, carton dimensions, units per carton, cartons per pallet. Two purposes: it confirms the freight quote was based on real figures, and it catches short-packing before the container seals.
Barcode scan verification. Physically scan retail barcodes on a sample from each carton type. A printed barcode that does not scan is a full repack at destination and it is entirely invisible to a visual inspection.
What a PSI cannot do is replace laboratory testing. Food-contact migration testing under EU Regulation 1935/2004 and the relevant LFGB methods, formaldehyde emission testing on any engineered panel component, and heavy metal testing on coloured finishes all require a lab and a separate sample submission. Those are one-time or annual exercises tied to the product, not per-shipment checks. The inspection report should reference the lab certificate; it should not pretend to substitute for it.
Writing The Inspection Clause So The Report Means Something
An inspection report that arrives after the container has sailed is a document, not a control. The clause has to tie the result to a payment or shipping event, and it has to say what happens on a fail. The mechanics that matter:
- Inspection precedes the balance payment or the shipping release. Under a 30/70 structure the balance is due against a passed PSI report plus the standard documents. Under an LC, the passed report is a required presentation document. This is the entire source of leverage and without it the rest is advisory.
- Booking lead time and factory obligation. The factory books the inspection at least seven working days before the intended stuffing date and notifies the buyer of the booked date. A factory that “forgot to book” and now needs to ship has engineered a waiver.
- Who pays. Buyer pays the first inspection. The factory pays every re-inspection caused by a failed result. This is standard, accepted across Vietnamese wood factories, and it changes behaviour more than any other clause in the paragraph.
- What a fail triggers. Name the options explicitly: 100 percent sorting at factory cost with re-inspection, rework with re-inspection, an agreed discount for a documented and quantified condition, or cancellation of the affected SKU. Without this list, a fail becomes a negotiation from zero.
- Pending result handling. A “pending” outcome, common when the inspector finds a documentation gap rather than a product defect, has a defined correction window, typically 48 hours, after which it converts to a fail.
- Access. The buyer or the buyer’s representative may attend any inspection, and the agency reports to the buyer directly, not through the factory. Reports that arrive forwarded from the factory email have been read first.
One detail buyers frequently miss: the inspection booking must reference the approved sample by its physical identifier, the sealed sample number and date, not by a description. Inspectors compare goods to a physical reference. If no sealed sample exists at the factory, the inspection is a check against a spec sheet, which is a much weaker instrument on a product where appearance carries most of the value.
What Inspection Costs And When It Pays For Itself
Third-party inspection in Vietnam in 2026 prices at roughly USD 280 to 400 per man-day for the recognised international agencies, with regional and local agencies sitting closer to USD 180 to 260. A standard PSI on a single-SKU wooden kitchenware order is one man-day. A mixed container with six to eight SKUs is typically two man-days because the sample count multiplies with each lot. Add a travel surcharge of USD 50 to 100 if the factory sits outside the Ho Chi Minh City, Binh Duong or Dong Nai corridor, which most wood factories do not.
Set against that, the arithmetic of a failed container is straightforward. On a 20ft container of wooden kitchenware with an FOB value around USD 45,000 to 60,000, a 10 percent defect rate discovered at destination costs the value of the affected units, plus destination handling on goods that cannot be sold, plus either a return shipment nobody wants to pay for or a disposal cost, plus the retail channel consequence, which is usually the largest and least recoverable item. The inspection is under one percent of the order. It does not need to catch much to pay for itself.
The less obvious return is behavioural. A factory that knows every shipment is inspected, and that it pays for re-inspections, manages its own quality upstream. The inspection changes what happens on the production floor in the weeks before the inspector arrives, which is worth considerably more than the findings in any single report.
Frequently Asked Questions
Can I use the factory’s own QC report instead of a third party?
On a mature relationship with a proven factory, internal QC reports are useful operational information and worth asking for on every shipment. They are not a substitute for independent inspection on the shipments where money is at stake, because the report cannot serve as evidence in a claim that the report’s author is party to. A reasonable middle position on established programmes is internal QC on every shipment plus third-party PSI on a defined proportion, say every third shipment and any shipment containing a new SKU.
How far in advance should I book a pre-shipment inspection?
Seven working days is the safe minimum, and agency availability tightens sharply in the weeks before Tet and before the Q4 shipping rush. Book earlier for inspections falling in January, and remember that Vietnamese factories often produce ahead of Tet and hold goods, which means your inspection date may need to sit well before your stuffing date.
What happens if the inspection fails and the shipping window is already tight?
This is why the fail options need to be written down before the order runs. In practice the fastest route is 100 percent sorting at the factory, which on wooden kitchenware can usually be completed in two to four days on an order under 20,000 units, followed by a partial re-inspection of the sorted lot. Shipping a failed lot under a written waiver is sometimes the commercially correct decision, but the waiver must be specific to the identified defect, quantified, and tied to an agreed discount. A general waiver is the same as having no inspection clause.
Should moisture content be tested at inspection or at the factory’s own kiln?
Both, and the two readings answer different questions. The kiln record tells you the wood was dried correctly. The inspection reading tells you what the finished, packed product is carrying after machining, finishing and time in a humid warehouse, which is the figure that determines whether it survives the destination climate. Ask for kiln records as part of the documentation pack and insist on independent meter readings in the PSI.
Is container loading supervision worth adding to a PSI?
On a mixed container with multiple order references, yes, because the risk is not product quality but wrong quantities and wrong cartons in the wrong load. On a single-SKU floor-loaded container from a factory with a clean loading history, it is usually an unnecessary second man-day. If you have ever received a short shipment from a factory, add it and keep it.
Working With Viet Farm Vision
Viet Farm Vision works with importers, retail groups and distributors sourcing wooden kitchenware and houseware, handmade quilling cards and eco packaging from Vietnam. Inspection is built into how we structure an order rather than added when something goes wrong. For buyers running a wooden kitchenware programme that means:
- A defect classification table drafted for your specific SKUs and retail channel, agreed with the factory before the order is quoted rather than after a dispute
- Sealed reference samples and colour range samples held at the factory and documented, so inspections compare against a physical standard
- Moisture content bands set against your destination climate, not the factory’s default
- Inspection booking managed on schedule, with reports issued directly to you by the agency
- Clear fail handling agreed in the PO, including who pays for re-inspection
Related reading: annual price agreements for Vietnam wooden kitchenware, mixed containers and consolidated orders, and warehousing and stock rotation after the container lands. External reference: the ISO 2859-1 sampling standard.
If you are planning a 2026 wooden kitchenware programme and want the inspection framework set up before the first PO rather than after the first claim, we are happy to walk through it. Contact us at info@vietfarmvision.com or through the enquiry form on vietfarmvision.com.